SUNDI TOOLS
- Copyright © Wuxi Sundi Precision Tools Co.,LTD All rights reserved.
- Site Map
 Skip to content
Choosing a Chocopie Cake Production Line is a practical decision, not merely an equipment purchase. The line must shape soft cakes, apply filling evenly, coat each piece smoothly, and protect product quality during packing. Every stage matters.
Joseph M. Juran, a respected quality-management expert, said, “Quality does not happen by accident.” His principle applies directly to Chocopie production. A reliable line needs controlled baking temperatures, accurate depositor settings, stable chocolate flow, and hygienic conveyor design. Small variations can create cracked shells, uneven cream, or dull coatings. These defects may appear minor, but customers notice them immediately.
This guide examines the details buyers often overlook. Production capacity should match realistic orders, not optimistic forecasts. A line rated for 20,000 pieces per hour may perform differently with specific cake formulas and coating thicknesses. Ask suppliers for test results using your ingredients. Check changeover time, cleaning access, spare-part availability, and operator training. Energy use also deserves attention.
Do not choose the fastest machine automatically. Speed without consistency can increase waste. A cheaper line may later require expensive modifications. That risk is easy to underestimate.
Experience matters here. Visit an operating factory if possible. Watch the cake release, filling control, and packaging alignment. Record actual observations, not only sales promises. The perfect line may not exist, but the right Chocopie Cake Production Line should deliver repeatable quality, manageable maintenance, and room for future growth.
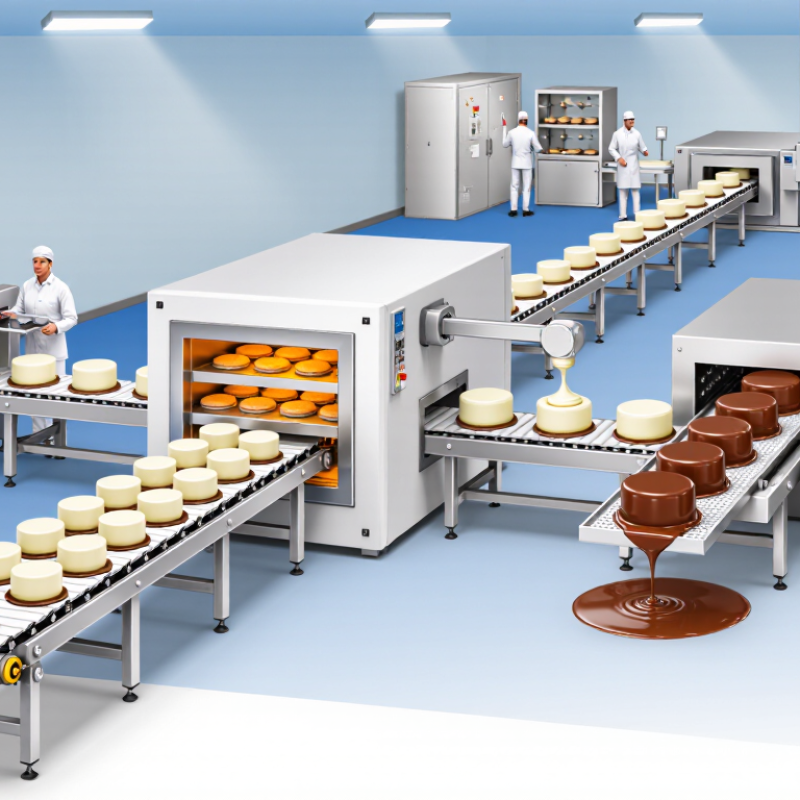
Before choosing a Chocopie cake production line, define the product precisely. Record cake diameter, filling weight, chocolate coating thickness, moisture target, and daily output. A 45-gram cake needs different depositing and cooling settings than a 70-gram cake. Specify acceptable variation, too. For example, keep piece weight within ±2 grams during pilot production.
Food safety must shape the design. The WHO recommends keeping free sugars below 10% of daily energy intake, with further benefits below 5% (Guideline: Sugars Intake for Adults and Children, 2015). This does not dictate your recipe, but it encourages clear formulation goals. Set allergen controls, sanitation intervals, metal detection, and traceability before requesting equipment quotations. ISO 22000 principles can help structure these controls.
Capacity targets should include real losses, not only ideal machine speed. FAO reported that 14% of food was lost between harvest and retail globally (The State of Food and Agriculture, 2019). Cake production also loses pieces through trimming, filling errors, coating breaks, and rejected packaging. Allowing a 3–5% operational loss may be more honest than promising full output. I would test a line with actual cream viscosity and packaging materials. Laboratory trials can look perfect. Factory conditions rarely do. Define changeover time, labor limits, energy use, and future product sizes before selecting the forming, baking, cooling, coating, and packing modules.
| Planning Dimension | Requirements to Define | Example Planning Target | Production-Line Implication |
|---|---|---|---|
| Product format | Shape, number of cake layers, filling type, coating, and whether the product is individually wrapped | Two soft cake layers with a marshmallow-style filling and an external chocolate-flavored coating | Specify depositing, sandwiching, coating, cooling, and wrapping equipment to match the intended product construction |
| Product dimensions | Target diameter or length, height, and allowable variation | Define dimensions through product trials; a compact single-serve format may be around 50–70 mm across | Size affects moulds, transfer spacing, coating coverage, cooling time, and packaging dimensions |
| Unit weight | Target net weight and acceptable production variation | Set a nominal weight based on the intended serving and pack size; verify it with repeated pilot runs | Use controlled batter and filling deposits, with checkweighing to monitor finished packs |
| Line capacity | Required saleable output per hour or shift, not just the machine’s nominal speed | Establish low, expected, and peak demand scenarios before selecting a line rate | Capacity must account for product losses, changeovers, cleaning, stoppages, and the speed of the slowest process step |
| Operating schedule | Shifts per day, production days per week, and planned changeover frequency | Document the expected schedule and available time for sanitation and maintenance | Operating hours determine required throughput and whether parallel equipment or buffer conveyors are needed |
| Cake process | Batter preparation, depositing method, baking profile, and cooling requirements | Set baking temperature and residence time through recipe and oven trials; confirm uniform bake and moisture | Choose an oven and depositor that can maintain consistent cake dimensions and provide adequate cooling before filling |
| Filling and assembly | Filling composition, deposited quantity, temperature, and sandwich alignment | Define filling texture and target deposit by product testing, including performance at the intended line speed | Filling equipment should deliver repeatable portions without damaging the cake or causing product slippage |
| Coating and cooling | Coating formulation, coverage, appearance, and cooling conditions | Specify acceptable coating coverage and finish; validate coating temperature and cooling time with the chosen recipe | Allow sufficient enrobing capacity and cooling-conveyor length to set the coating before handling and wrapping |
| Packaging format | Individual wrap, multipack configuration, film type, and coding requirements | Choose pack count and package dimensions based on sales format and distribution needs | Match the wrapper’s rated speed and sealing method to product size, film properties, and line output |
| Shelf-life goal | Target shelf life, storage conditions, and product-quality limits | Determine shelf life through validated testing of the finished recipe and packaging under defined storage conditions | Packaging barrier properties, seal integrity, recipe, hygiene, and storage conditions all affect shelf life |
| Food safety and quality | Allergen controls, sanitation, traceability, inspection, and applicable local requirements | Identify allergens in the recipe and establish documented cleaning, monitoring, and batch-traceability procedures | Include suitable inspection and control points; equipment layout should support hygienic access and cleaning |
| Facility and utilities | Available floor space, electrical supply, compressed air, water, drainage, and ventilation | Confirm site capacities and connection points before finalizing equipment specifications | Request utility consumption and layout drawings for the complete line, including ovens, cooling conveyors, and packaging |
| Flexibility and growth | Potential recipe, size, pack-format, and output changes | List likely product variants and forecast capacity needs over the planned equipment life | Prioritize adjustable settings, accessible change parts, and expansion space where future changes are likely |
| Investment goals | Budget, labor availability, automation level, and expected operating costs | Compare equipment using total cost of ownership, including labor, energy, maintenance, waste, and downtime | Balance automation and line speed against product mix, service support, and the facility’s operating capability |
Planning figures and example specifications should be confirmed through recipe trials, packaging tests, food-safety review, and a site-specific line assessment before equipment is purchased.

 English
 Russian
 German
 Spanish
 French
 Portuguese